Hey there, if you’ve ever been deep in a production plant watching a chain plate feeder chain trudge along a super long conveyor line—say, moving raw materials or finished parts 100+ meters from one end to the other—you know the pain when it starts acting up. It’s not just a little glitch; it can halt your whole operation, make you miss deadlines, and eat into profits way faster than you’d expect. Let’s cut the jargon and get real here, because as a chain plate feeder chain supplier, I’ve heard every horror story from plant managers who’ve dealt with this exact issue: that creaky, jolty chain that starts skipping teeth, wearing out way too fast, or even snapping mid-run. Long-distance conveyors put way more stress on these chains than short, looped ones, so you can’t just install ‘em and forget ‘em. Today, I’m walking through what actually works to keep that chain running smooth mile after mile (or whatever your long haul is—no need to stick to industry standard numbers, I get every line is different). Chain Plate Feeder Chain
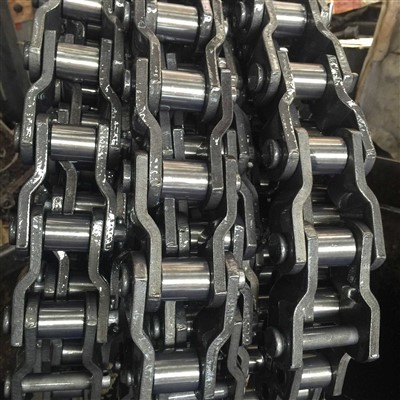
First off, let’s be clear: a chain plate feeder chain for long-distance runs isn’t the same as the ones you see on small conveyors. Short runs have less stretch, less load, and less room for error, but when you’re moving something across a whole warehouse or processing floor, the chain has to handle consistent tension, side load, and even temperature changes that throw everything off. I’ve seen plant guys install the wrong type of chain for their long setup—like a standard roller chain instead of a self-lubricating double-pitch plate chain—and wonder why it dies in six months. That’s not a "bad chain" thing, that’s a mismatch. So first rule: pick the right chain for long distance, not just whatever fits your sprockets.
Wait, let’s talk tension first, because that’s the biggest culprit for long runs. If your chain is too loose, it’s gonna sag between the sprockets, right? That sag causes side rub against the conveyor frame, makes the chain jump when it goes around the bends, and over time, wears down the plate links way faster. But if it’s too tight? Oh man, you’re putting unnecessary stress on every single link, the bearings seize up, and you’re looking at a premature break. I’ve had a client tell me they tightened their chain so much to stop sag that it snapped 2 weeks later—because the tension was pulling the links apart under the constant load of a 150-meter line. So how do you get that tension right for long-distance setups? It’s not as simple as "pull it until it doesn’t sag." You need to adjust for the load: if you’re moving heavy bulk materials, you need a slightly higher tension, but you have to do it gradually, not yank it. Also, check the sag at the midpoint of the conveyor—for long runs, the midpoint sag should be about 1-2% of the conveyor span. Wait, let’s make that simple: if your conveyor is 100 meters long, midpoint sag shouldn’t be more than 1 or 2 meters. That’s a rule of thumb that works, no fancy math needed. And here’s a pro tip from my team: don’t just set it once. Every month, check the tension, especially when you’re switching between loads. If you run light one week and heavy the next, that sag will change. Tension adjustments aren’t a "set it and forget it" job—especially for long lines.
Next up, lubrication. If you think lubrication’s just spraying some oil on the chain now and then, you’re dead wrong for long-distance runs. These chains are moving nonstop, sometimes 24/7, so the right lubricant and the right application method make all the difference. I’ve seen plants use regular motor oil, which dries up in a day when the chain is spinning constantly and exposed to dust or debris from whatever they’re moving. For long-distance chain plate feeder chains, you need a lubricant that’s adhesive—meaning it sticks to the links and pins, not just slings off when the chain moves. Also, the amount matters: too little, and friction wears out the pins and bushes; too much, and it attracts dust, which acts like sandpaper grinding down the links.
Here’s what works for my long-distance clients: automatic lubrication systems, not manual spray bottles. Manual is fine for short runs, but when your chain is 100 meters long, manually spraying every few hours is a waste of time and you’re gonna miss spots. Automatic systems can be set to apply a consistent, thin coat of lubricant exactly where it’s needed—usually at the upper return side of the chain, where most of the friction happens. And pick the right lubricant type: if you’re in a plant with high temperatures (like a metal foundry), use a high-temperature synthetic lubricant; if you’re moving food or pharmaceuticals, use a food-grade lubricant that’s safe even if it drips a little. I can’t tell you how many times I’ve gotten a call from a food processing plant saying their chain is squeaking, and it turned out they were using the wrong lube that would’ve contaminated their product. Don’t skip this step—lubrication is 50% of keeping that chain smooth.
Then there’s alignment. This is another big one that people overlook, especially with long conveyors. If the sprockets at each end aren’t perfectly aligned, or the conveyor frame is slightly bent, the chain will pull to one side every time it runs. Over time, that side rub causes uneven wear on the chain plates, and it can even bend the sprockets. For long-distance runs, alignment isn’t just a quick check with a level. You need to do a "chain walk" check: run the conveyor for 10 minutes, stop it, and see if the chain is sitting centered on the sprockets on both ends. If it’s drifting left or right, adjust the sprocket mountings a little. Also, check the guide rails on the conveyor—those are the little rails on each side that keep the chain from shifting. If they’re worn down or misaligned, the chain will rub against them, creating friction and making that annoying creaky noise that’s the first sign of trouble. I had a client with a 200-meter conveyor who thought the chain was just bad, but it turned out one guide rail was 3mm off, causing the chain to wear on one side so bad it needed replacement 2 months early. Alignment isn’t a one-time thing either—vibration from constant running can shift sprockets or frames, so check alignment every quarter, or after any major maintenance on the conveyor.
Wait, let’s talk about load distribution too, because long-distance conveyors often carry more material further along. If you’re dumping all your load at one end, that puts way more stress on the first half of the chain, making it stretch unevenly. Instead, spread the load as evenly as possible along the conveyor line. Some plants use multiple feed points along the long conveyor, which takes pressure off the early links and keeps the chain stretching uniformly. Also, avoid overloading the chain—even if it’s rated for a certain weight, a long run means the total load is more, so make sure you don’t exceed the chain’s maximum working load. I’ve seen guys overload a chain just to get more product through, and within a month, the links are starting to elongate, making the chain skip on the sprockets. Elongation is a natural part of chain wear, but uneven elongation from overloading or bad tension is what causes all the problems.
Another thing that’s super important for long runs: regular inspection of the chain links and sprockets. You can’t wait until the chain breaks to check it. Set a schedule: every week, do a quick visual check of the tight spots, especially around the sprockets, for any broken links, bent plates, or worn sprocket teeth. Every month, check for elongation: measure a 10-link section of the chain, if it’s stretched more than 2% of its original length, it’s time to adjust tension or replace sections. For long conveyors, don’t wait for the whole chain to go bad—replace worn links in sections, because if you wait, the worn links will cause the good ones to wear faster too. I always tell clients: small, regular checks are way cheaper than a full chain replacement or a day of downtime when your whole line stops.
Wait, what about environmental factors? Like, if your conveyor is outside, exposed to rain, snow, or extreme heat? That changes things a lot. For outdoor long-distance conveyors, you need a chain plate feeder chain with corrosion-resistant coating—like zinc plating or stainless steel, instead of standard carbon steel. Rain will cause rust, which makes the links seize up, and snow or ice will add extra load, so you have to check tension more often and maybe use a thicker lubricant for cold weather. I had a construction client with an outdoor conveyor that kept rusting the chain during rainy season, and switching to a coated chain fixed that problem completely. They no longer had to replace the chain every 6 months, it lasted 2 years instead.
Let me also bust a common myth here: a lot of people think "higher quality chain means no problems." Nope, even the best chain needs proper care. I sell top-quality chain plate feeder chains, but I’ve seen clients install a $5000 chain and only lubricate it once a year, and it dies in a year. Conversely, I’ve had clients with our standard mid-range chain that’s properly maintained and adjusted, running smooth for 5+ years on a 120-meter line. Quality is part of it, but maintenance and setup are way bigger for long runs.
Wait, let’s recap so it’s easy to follow, no fancy steps: first, make sure you’re using the right chain for long distance—self-lubricating, corrosion-resistant if needed, double-pitch for heavy loads. Second, get the tension right, not too loose not too tight, check the midpoint sag every month. Third, use automatic, consistent lubrication with the right type for your environment. Fourth, keep sprockets and guide rails perfectly aligned, check alignment quarterly. Fifth, spread your load evenly along the conveyor, don’t overload it. Sixth, do regular small inspections—weekly visual checks, monthly elongation measurements. Seventh, adjust for environmental factors (corrosion, temperature, outside exposure).
Now, if you’re reading this and thinking, "Ugh, my long conveyor’s acting up and I don’t know where to start," that’s exactly why I’m here. As a chain plate feeder chain supplier, I don’t just sell chains— I help you figure out what’s gonna work for your specific long-distance setup, not just give you a generic product. I’ve worked with plants of all sizes, from small warehouses to big manufacturing facilities, and every time, the same principles apply: proper setup, consistent maintenance, and picking the right parts for your line.

If you’re tired of that jolty chain, unexpected downtime, and constant replacements, hit me up to talk through your conveyor setup. We can go over your line length, load type, environment, and figure out exactly what you need to keep that chain running smooth for the long haul. No pushy sales talk, just real advice from someone who works with this stuff every day.
Chain References:
- Machinery’s Handbook. Industrial Press, 2020.
- Chain Drive Design and Application Guide. American Chain Association, 2019.
- Conveyor Maintenance Best Practices for Long-Distance Systems. Material Handling Industry Association, 2021.
Zhejiang Hangte Chain Transmission Co., Ltd.
We are one of the most experienced chain plate feeder chain manufacturers and suppliers in China since 1999. Please rest assured to buy high quality chain plate feeder chain made in China here from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: No. 195 Qinglin East Street, Qingshan Lake Subdistrict, Lin’an District, Hangzhou City, Zhejiang Province
E-mail: hangtechain@gmail.com
WebSite: https://www.chinahtchain.com/
