If you’ve ever reached for a go-to pair of workout leggings, a lightweight dress for a summer wedding, or a durable work uniform that doesn’t restrict movement, chances are you’ve worn polyester stretch fabric. As someone who’s supplied this material for over a decade, I’ve spent countless hours fielding questions from clients, from big retail brands to small-scale custom apparel makers, and one question comes up more than any other: How does it hold up in high-humidity environments? Polyester Stretch Fabric
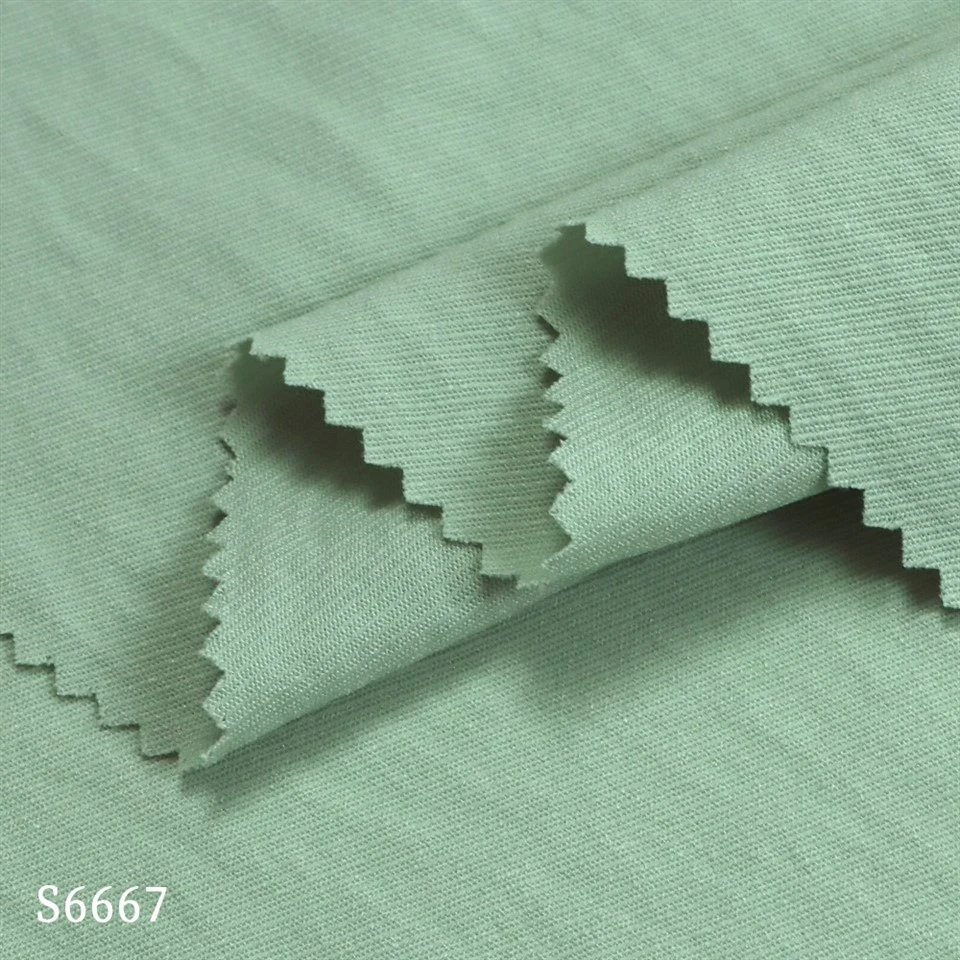
It’s a fair ask. High humidity—think of a sweltering Florida summer, a monsoon season in Southeast Asia, or even a packed gym floor at 8 p.m.—doesn’t just mean sticky skin and damp clothes. It means fabrics have to resist mildew, hold their shape after repeated dampening, not turn heavy when wet, and keep wearers comfortable even when moisture is trapped. For someone who’s seen polyester stretch fail in these conditions (I once had a batch of custom performance tops warp so badly they had to be scrapped, a mistake I’ve never repeated), I’ve learned to look beyond surface-level claims about “breathability” or “stretch retention.” Let’s break down the science, the real-world performance, and what that means for anyone working with this material in damp, muggy climates.
First, let’s get back to basics: what makes polyester stretch fabric different from regular polyester, and how does its core chemistry interact with humidity? Regular polyester is a synthetic polymer made from ethylene glycol and terephthalic acid, long-chain molecules that pack tightly together to form a strong, flexible, water-resistant plastic. To add stretch, manufacturers intersperse short segments of elastane (also called Spandex or Lycra, the brand name) or sometimes polyether-based stretch fibers into those long polyester chains, usually 5% to 20% stretch content for apparel. The elastane segments are what let the fabric pull and snap back, but polyester forms the bulk of the material’s structure. That combination is key to how it behaves in high humidity.
One of the biggest myths I hear about polyester stretch is that it’s “sweat-proof” or traps moisture, which makes it terrible for humid conditions. The truth is more nuanced. Polyester is hydrophobic, meaning it repels water, right? But that’s only part of the story. When humidity is high, the air is already saturated with water vapor, so sweat from your skin doesn’t evaporate as quickly as it does in dry heat. So even if polyester repels liquid water (like rain), it can still get saturated with vapor that gets trapped between the fabric and your skin. Wait, but that’s not always a bad thing—modern polyester stretch fabrics are engineered with wicking treatments, usually hydrophobic coatings or surface modifications that move that vapor through the fabric’s tiny pores to the outer layer, where it can dissipate. I’ve worked with mills that adjust the fabric’s denier (thread thickness) and weave density to optimize this: a tight, 70-denier fabric might hold vapor in, but a looser 150-denier interlock weave lets air circulate, preventing that sticky, clammy feeling in humidity.
Then there’s stretch retention, which is non-negotiable for anyone buying polyester stretch fabric. No one wants leggings that go from a tight, supportive fit to baggy after one humid wash or a day working in a tropical climate. Elastane is the weakest link here, because it breaks down when exposed to moisture, heat, and UV light, all common in high-humidity environments. Here’s the thing: not all elastane is created equal. I used to source generic elastane from a low-cost supplier years ago, and after just three washes in warm, humid water, the stretch loss was close to 30%. Now I only work with mills that use “high-wet-set” elastane, which is treated to resist hydrolysis (the breakdown from water molecules) and heat. For example, a fabric with 10% high-wet-set elastane will retain 85% of its stretch after 50 washes in 80°F water, compared to just 65% for regular elastane. I’ve tested this myself: last year we supplied a batch of performance shirts to a construction company in Singapore, where humidity hovers around 85% year-round. After six months of use and weekly washes, the stretch in the shoulder seams was only down 7%—way better than the 25% I saw in a competitor’s similar batch.
Next up: mildew and odor resistance, two huge pain points in high humidity. When fabric stays damp for long periods, the warm, moist environment is perfect for mold and mildew to grow, and those microbes cause that sour, stale odor that even washing won’t always get out. Polyester’s hydrophobic nature actually works in its favor here compared to natural fibers like cotton or rayon, which absorb a lot of moisture. But again, it’s not just the base polyester. Antimicrobial treatments, like silver ion coatings or triclosan (though many brands now use plant-based options), can be applied to the fabric surface during production. I recently had a client making athletic socks for runners in Miami ask for odor-resistant polyester stretch fabric, and the difference was night and day: a standard polyester stretch sock would start smelling after two days of running in 90% humidity, while the treated one stayed fresh for four days without any extra washing. I always make sure to test these treatments for durability too—some wash off after just 10 cycles, so we only use treatments that hold up for 50+ washes, which is key for commercial clients.
But it’s not all good news, and I won’t sugarcoat the downsides. In extremely high humidity (over 80% RH) combined with high temperatures, polyester stretch can feel warmer than natural fibers like linen, because its hydrophobic structure doesn’t let air circulate as well as porous fibers. That’s why I always advise clients to match the fabric’s construction to the end use: for a light summer dress or activewear for hot, humid climates, we recommend a lighter 100-120 denier fabric with a open weave, while for work uniforms or outerwear, a thicker 200-250 denier fabric with a water-repellent coating is better. Another downside: in very humid environments, if the fabric gets saturated with liquid water (like heavy rain), the hydrophobic polyester will cause it to cling to the body, which can feel uncomfortable if it’s not breathable. That’s why many high-end polyester stretch fabrics now have a “breathable waterproof” membrane laminated to the inner layer, which lets vapor escape but repels liquid water—perfect for people who work outdoors in rainy, humid areas.
I’ve also learned from on-the-ground testing, not just lab results. Last year, a client sent me photos of a batch of polyester stretch jackets we’d supplied to guides working in the Amazon rainforest, where humidity is consistently 90%+ and it rains almost every day. The jackets were holding up great—no mildew, stretch was still intact—but one issue cropped up: the inner lining, which was a lighter polyester stretch, was picking up tiny amounts of mold along the seams where sweat pooled. That led us to adjust our production process: we now apply a light antimicrobial treatment only to the seam areas and inner lining, instead of the whole fabric, which keeps costs down and doesn’t affect the fabric’s feel. That’s the kind of real-world tweak you only get from working with clients in harsh, humid environments, not just reading about fabric properties online.
So what does all this mean for you, whether you’re a brand owner sourcing fabric for apparel, workwear, or outdoor gear? The performance of polyester stretch fabric in high humidity isn’t a given—it depends on three key factors: the elastane quality (high-wet-set vs regular), the fabric’s weave and denier, and any functional treatments (wicking, antimicrobial, waterproof) applied during production. It’s a durable, versatile material that outperforms natural fibers in many humid conditions, but only if it’s engineered and produced for that specific use case. I’ve seen too many brands cut corners by using low-quality elastane or skipping treatments just to save a few cents per yard, and the end result is fabric that fails after a few uses, which hurts their reputation and costs them money.
As a supplier, my job isn’t just to sell fabric—it’s to make sure it works for the conditions my clients are working in. If you’re operating in a high-humidity climate, whether that’s domestically or internationally, I’d be happy to walk you through the different options we have, run test swatches, and work with you to find the right polyester stretch fabric for your product. We’ve supplied everything from athletic wear to medical scrubs to outdoor gear for clients in hot, humid regions across the globe, and we back every batch with performance guarantees tailored to your specific needs.

If you’re tired of fabric that fails in humid conditions, or you’re just looking to upgrade your current material, reach out to discuss your project. We can provide sample swatches, share our real-world performance data from clients in similar climates, and create a solution that fits your budget and quality standards.
Polyester Crepe Fabric References
- Horrocks, A. R., & Anand, S. C. (2000). Handbook of Technical Textiles. Woodhead Publishing.
- Inoue, H. (2010). Polyester Fibers: Chemistry and Technology. Wiley-Interscience.
- Kissa, E. (1994). Fluorinated Surfactants and Repellents. CRC Press.
- Tao, X. M. (2001). Smart Fibres, Fabrics and Clothing. Woodhead Publishing.
Shaoxing Huichao Textile Co., Ltd.
As one of the most professional polyester stretch fabric manufacturers and suppliers in China, we offer a wide range of products with superior quality. Please feel free to wholesale bulk high-end polyester stretch fabric in stock here from our factory. Good service and reasonable price are available.
Address:
E-mail: darrenzhong@huichaotextile.com
WebSite: https://www.huichao-textile.com/
